
Preview sample formats for CoC, CTQ inspection reports, and packaging checklists.
ISO 9001 QMS • Inspection evidence • Export-ready delivery
Quality Systems for Precision Machining in Vietnam
ISO 9001 QMS applied on the floor: contract review, controlled planning, calibration, in‑process gates, final inspection, corrective action, and receiving‑ready documentation.
Precision machining
5-axis capable
Inspection reports
Export-ready packaging
Proof
Evidence you can request at RFQ
A quality system should be visible in deliverables: gates, reports, decision rules, and corrective action. Start with these proof links.
Quality foundation
ISO 9001 discipline + practical manufacturing controls
International buyers evaluate more than “can you machine the part?” They evaluate whether your process reliably produces the same result at scale—and whether you can provide evidence for receiving and approvals.
SEMIX builds that reliability using a structured quality approach:
- Contract review to confirm revision level, CTQs (critical-to-quality), documents required, and packaging rules before production starts.
- Planning that defines datums, fixtures, tool strategy, measurement plan, and inspection checkpoints.
- In‑process controls that detect drift early and protect yield (especially for long cycle times).
- Final inspection aligned to engineering intent (GD&T) with reporting tailored to your receiving needs.
- Corrective action & continuous improvement to prevent recurrence and strengthen process capability.
Quality gates: where variation is detected and controlled
An engineering‑credible quality system is built around gates—defined checkpoints where risk is measured, decisions are made, and evidence is recorded. This is how a machining supplier becomes predictable across high mix, multiple shifts, and changing schedules.
| Gate | Purpose | Typical controls | Evidence |
|---|---|---|---|
| Incoming | Prevent nonconforming material/finish inputs from entering production | Material ID & certification review, visual condition checks, finishing boundary confirmation | MTR/heat cert traceability link, receiving record |
| Setup approval | Lock datums, clampings, and tool assemblies before running volume | First‑off checks, datum verification, fixture validation, critical tool offsets locked | Setup sheet, first‑off record |
| In‑process | Detect drift early (tool wear, thermal shift, fixture movement) | Sentinel feature checks, tool-life gating for finishing, SPC where appropriate | In‑process logs, trend snapshots |
| Final inspection | Verify requirements using a method aligned to CTQs and GD&T | Calibrated tools, CMM strategy where needed, sampling plan agreed to in contract review | Inspection report / CMM report, acceptance statement |
| Pack & ship | Prevent damage and receiving friction | Protective packaging, labeling/kitting checks, doc bundle verification | Packing checklist, document bundle |
Nonconformance & corrective action (closed-loop)
- Containment first: isolate affected parts and evaluate downstream impact before any disposition.
- Root cause by mechanism: distinguish tool wear drift, fixturing variation, programming assumptions, and measurement method issues.
- Corrective action: update the control plan (not only “retrain”)—route gates, inspection points, tool-life limits, or fixture constraints.
- Verification: confirm effectiveness with follow-up data (first-pass yield, trend stability, reduced rework).
Supplier quality and traceability
For global supply chains, quality is also a traceability problem. A good supplier can show what material and special processes were used, when they were used, and how the result was verified—without reconstructing history after the fact.
- Material traceability linking MTR/heat certs to the job traveler and finished part lots.
- Finish traceability for outsourced processes when used (standard, lot, and certificate mapping).
- Revision control to ensure the factory is building the latest released design.
Calibration and measurement governance
Engineering credibility depends on measurement credibility. A controlled calibration system ensures inspection tools remain traceable and suitable for the tolerance they are used to verify.
- Calibration schedule for critical gages and instruments, with records available when required.
- Fit-for-purpose selection: tighter tolerances require higher measurement resolution and lower uncertainty.
- Environmental awareness: temperature and stabilization rules applied when tolerances are tight.
Training, standard work, and repeatability
In a CNC environment, repeatability is built from standard work: consistent setup, consistent verification points, and clear reaction plans. This reduces dependence on individual operator “heroics.”
- Setup standards for datums, clampings, and first-off approval.
- Reaction plans when an in-process check trends toward a limit (tool change, offset strategy, hold for engineering review).
- Document control to ensure the shop builds the correct revision with the correct notes.
Quality metrics that matter in production
| Metric | Why it matters | What improvement looks like |
|---|---|---|
| First-pass yield | Measures how often parts meet requirements without rework | Stable processes with fewer inspection escapes and less touch time |
| Rework drivers | Identifies where the process is not robust | Fewer root causes repeated; control plan updated |
| On-time delivery | Supply chain reliability indicator | Fewer slips from material, finishing, or inspection bottlenecks |
| Receiving issue rate | Measures friction at the customer interface | Cleaner documentation packs and fewer interpretation disputes |
Configuration management (revision discipline)
One of the most expensive quality failures is building the correct part to the wrong revision. Engineering‑credible suppliers treat revision control as a system, not a reminder.
- Contract review locks the revision (drawing + model + applicable specifications) before production starts.
- Controlled distribution so the shop floor and inspection use the same released package.
- Change evaluation to determine if a revision triggers re‑approval, additional inspection, or documentation updates.
Supplier quality for special processes
Many machining programs include external processes (anodize, passivation, plating, heat treat, laser marking). Quality control extends across that supply chain through defined boundaries and certificate traceability.
- Finish boundaries defined early (standard/spec, masking rules, cosmetic zones, acceptance criteria).
- Certificate collection and mapping so each shipped lot is traceable to its special process lot.
- Receiving readiness: documentation is bundled so your team does not chase missing certs.
Audit readiness and transparency
For qualified suppliers, buyers often need confidence that controls exist—not just marketing claims. SEMIX is structured to support supplier evaluations with process descriptions, evidence examples, and clear ownership of quality responsibilities.
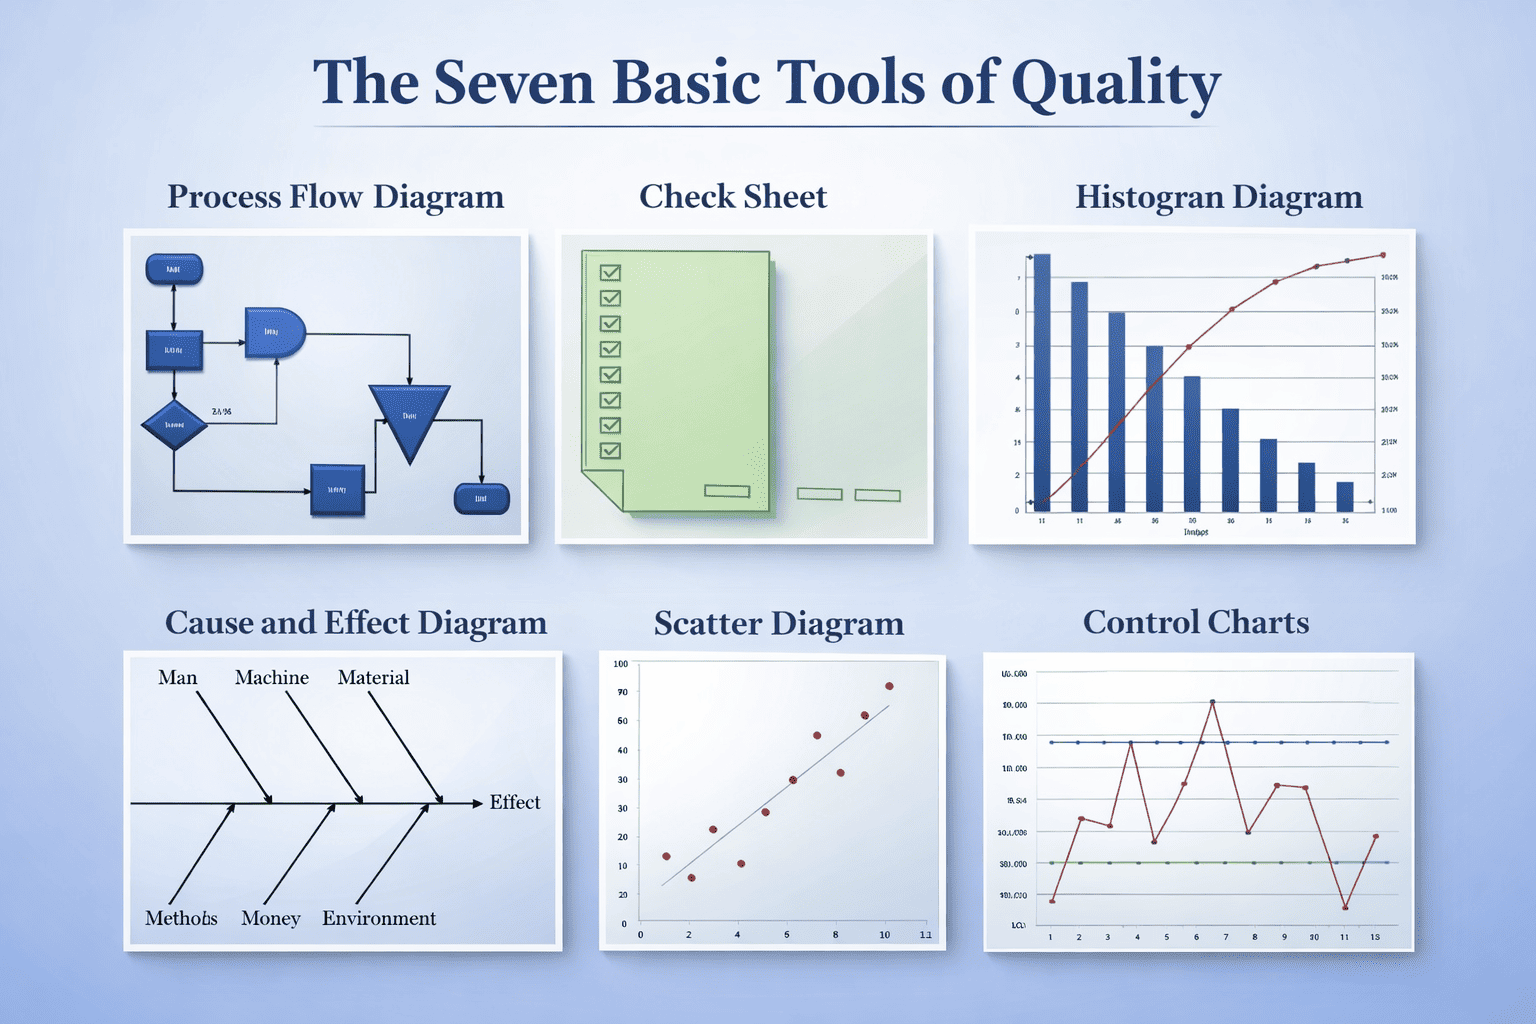
Inspection evidence
Inspection & metrology that supports approvals
Inspection is only useful when it answers the buyer’s question: “Can I accept these parts with confidence?”
We select measurement methods based on the part and CTQs:
- CMM / 3D measurement for dimensional and GD&T verification on complex parts.
- Vision measurement for small features and delicate geometry.
- Calibrated hand tools (micrometers, calipers, bore gauges, height gauges, surface roughness tools) under calibration control.
Need a specific reporting format? Tell us in the RFQ stage so we can plan measurement time, fixtures, and reporting methods.
Documentation
Documentation packages built for global receiving
Many delays happen after machining—at receiving and quality approval. SEMIX can prepare documentation packages that match your PO flow-down.
Certificate of Conformance (CoC), material certificates (when required), and basic dimensional report as specified.
Structured first-article style reporting (format based on your requirements), ballooned drawings, and measurement records as required.
Documentation samples (download)
Standardized, fill-and-print templates for CoC, traceability, travelers, inspection plans, packaging checklists, and controlled change communication.
CAPA / 8D template
A mechanism-based corrective action structure that links root cause to permanent controls and verification evidence.
FAQ
Quality & inspection: common questions
Are you ISO 9001 certified?
SEMIX operates an ISO 9001:2015 quality management system. You can review our approach and certification information on the ISO 9001 QMS page.
Can you provide CMM inspection reports?
Yes—when required by the PO/RFQ. Provide CTQs and reporting expectations early so we can plan metrology time and reporting structure.
How do you handle drawing revisions?
We confirm revision level during contract review and keep controlled records so production uses the correct data set. If revisions change mid‑stream, we align on impact to cost, schedule, and documentation before proceeding.
Do you support first-article packages (FAI)?
We can support first-article style documentation and measurement records based on your format/requirements. Please specify your expectations in the RFQ stage.
Leadership, facility, and metrology
These pages strengthen buyer trust signals (E‑E‑A‑T) and help procurement teams qualify SEMIX as a Vietnam CNC machining supplier.
Clear ownership for engineering, quality, and delivery decisions across global programs.
Location context, audit readiness, export-ready operations, and what buyers can request.
CTQ measurement planning and reporting that reduces receiving friction.
How we manage document control, nonconformance, and corrective actions.
CoC, MTR (as required), inspection reports, and first-article support.
Anonymized evidence showing workflow by industry.